
Holes that need re-drilling at assembly
When brackets come from rotating shops, each batch resets the tooling — hole positions drift and your fitters compensate on the line.
Solution · Sheet Metal Fabrication
A bracket is a simple part until hole patterns drift a millimeter between batches and your assembly line starts re-drilling. Our bracket workflow locks punch tooling, bend sequences and hole positions per project — verified on first articles before any batch ships.
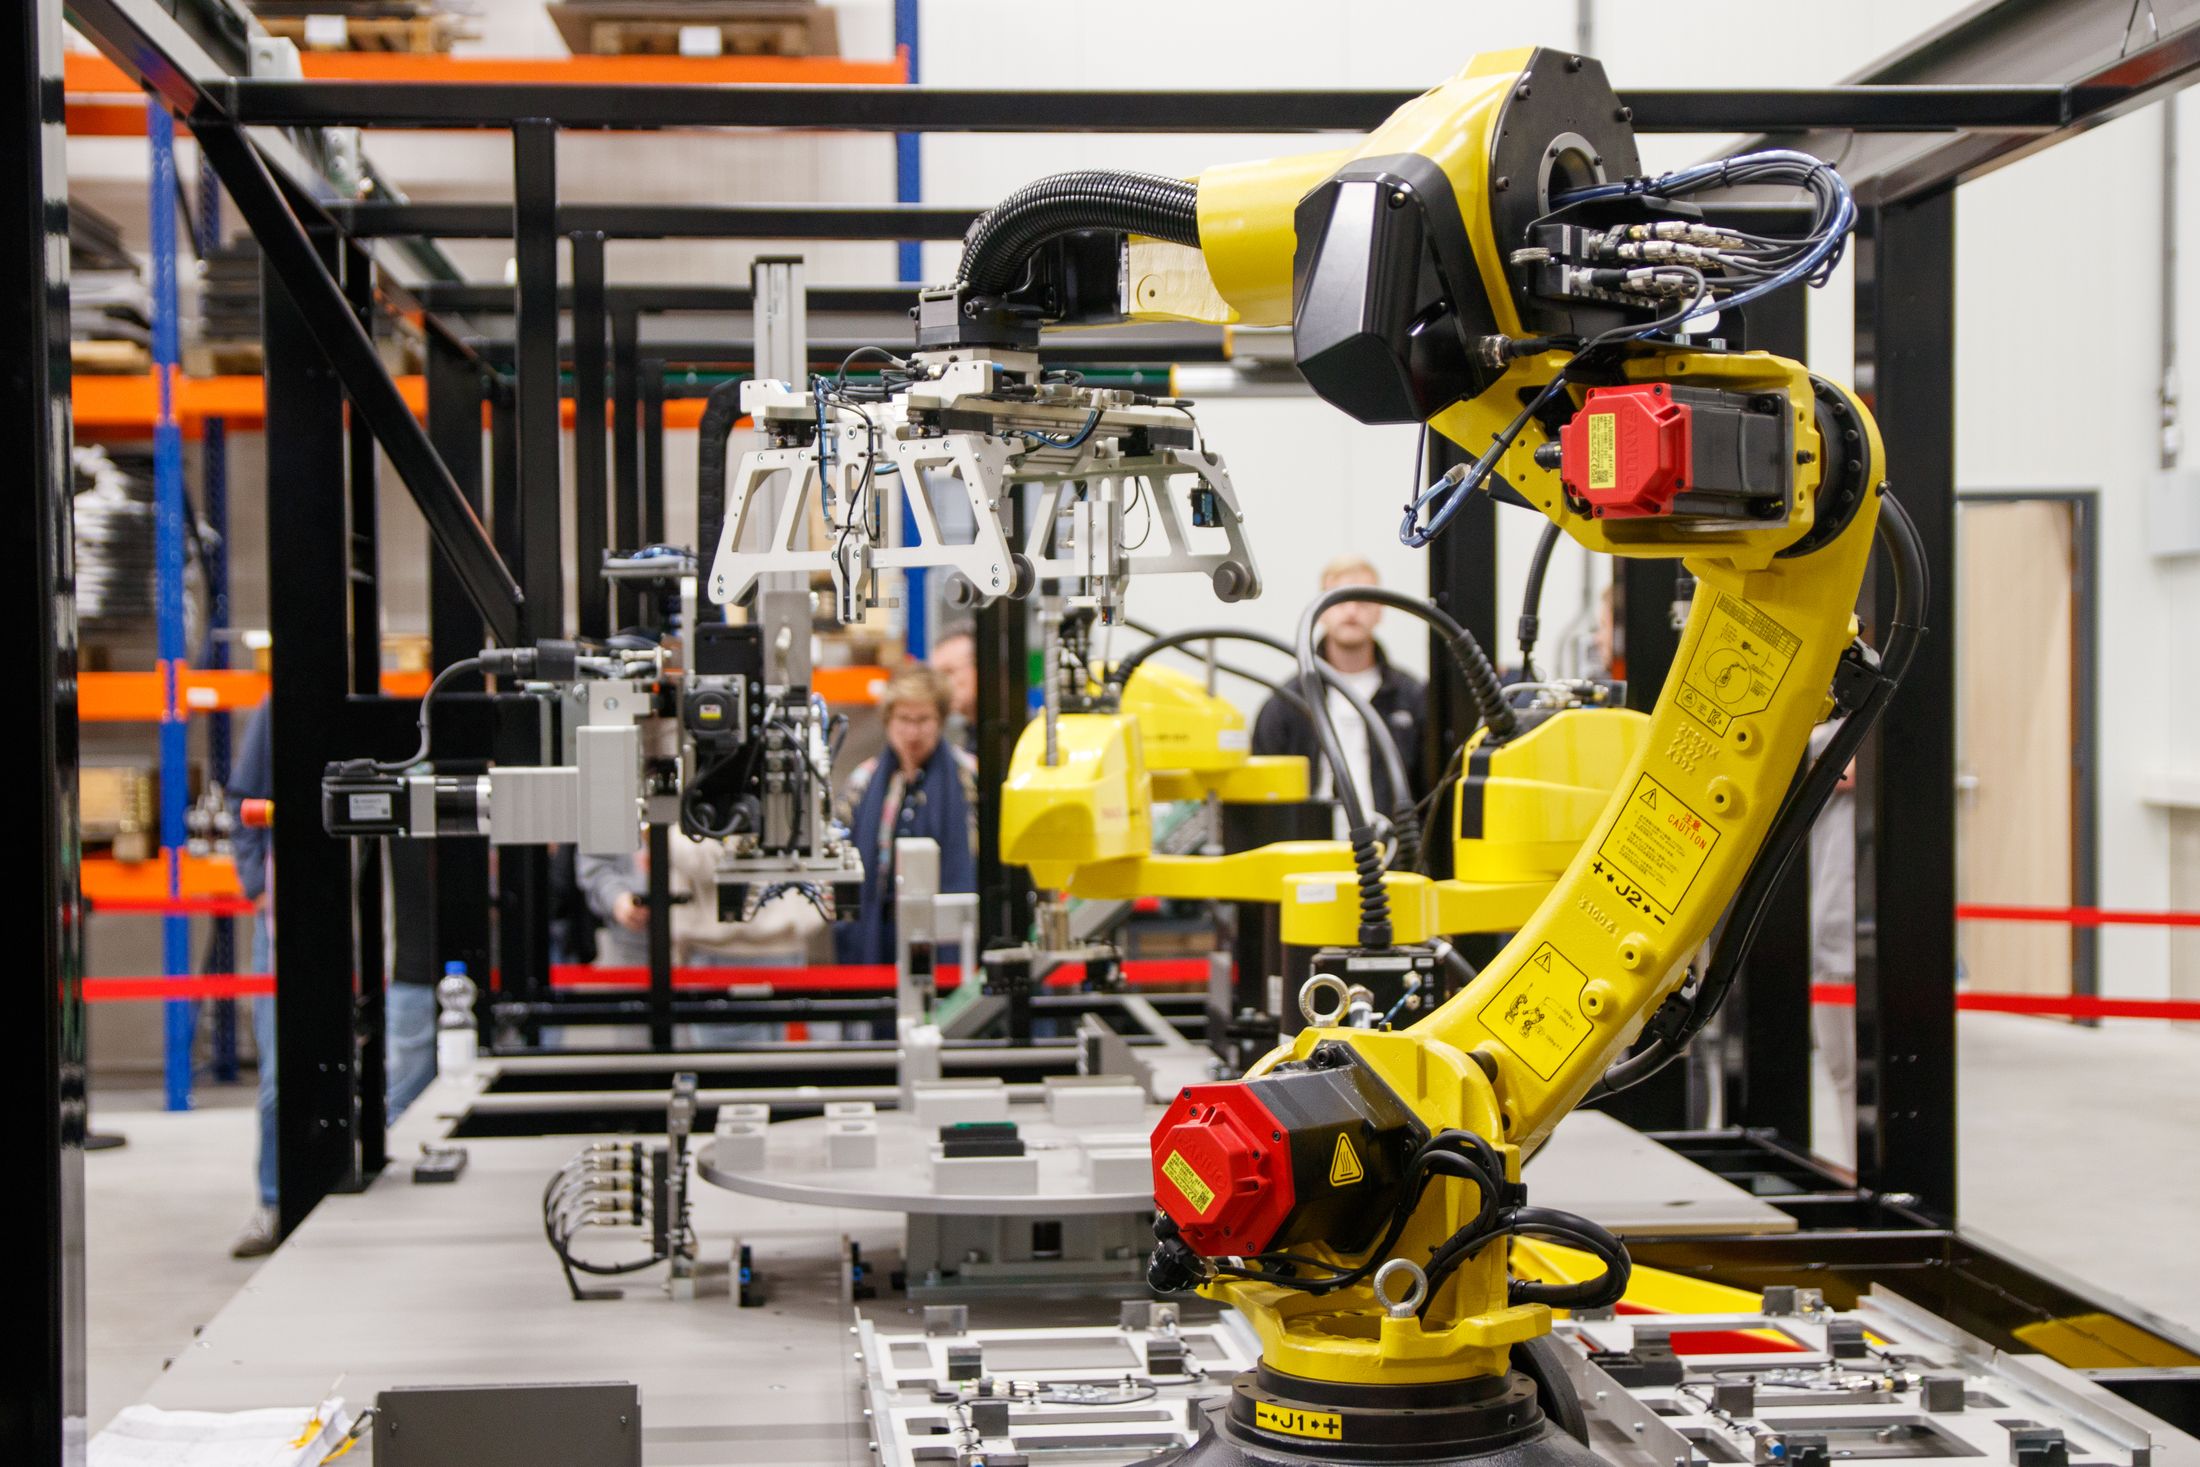
Forming accuracy
Press-brake bending with planned bend sequences and springback compensation.
Hole position control
Punch tooling and laser cutting hold hole patterns; positions verified on first articles.
Finish scope
Coating and surface expectations written into the inspection plan and quotation.
When brackets come from rotating shops, each batch resets the tooling — hole positions drift and your fitters compensate on the line.
Unplanned springback turns a 90° drawing into a batch of 88° brackets, and flat mating surfaces become shimming work.
Mild steel specified for a coastal or outdoor installation fails in the field — the cost lands on your warranty, not the supplier's.
Every bracket project starts with a drawing review where material, hole pattern, bend radii and finish scope are written into the inspection plan. Punch tooling and stored bend sequences hold geometry across batches, and first articles verify positions and angles before release.
TRUMPF TruMatic 6000 and Amada punching cut blanks and hole patterns from your drawings.
Press-brake bending with stored sequences and springback compensation keeps angles consistent.
Punch tooling per project holds hole positions across repeat batches without re-drilling.
Multi-part brackets and stiffeners welded by robot or hand, checked on first articles.
Select the material family and thickness range to see general bend-radius guidance used in bracket design. Final radii, springback compensation and tooling are confirmed at drawing review.
For 2–3 mm mild steel, plan for an inside bend radius around 1× thickness and a slight overbend to compensate springback.
Bend-radius guidance is a general engineering reference, not a bending guarantee. Final radii, springback compensation and tooling are confirmed at drawing review.
Typical application examples based on our documented workflow. Buyer roles are anonymized; outcomes depend on project specifics.
Buyer feedback examples framed around our standard documentation and workflow evidence; results reference checkable records.
“Hole patterns from the last four batches bolted straight on — our fitters noticed before we did.”
“Material certificates arrive with the shipment, which our site teams stopped questioning.”
“One inspection plan covers brackets and machined parts now, so freight and paperwork got simpler.”
Certifications below are held by Zhuhai ChunTian Machine Technology Co.,Ltd. Scope and validity details are available with the certificate documents on request.
Operating since 2009 with more than 15 years in precision sheet metal and CNC machining.
300–1,000 staff and an annual revenue of USD 30–150 million, running laser cutting, punching, bending, welding and machining under one roof.
Engineering team turns drawings into quote-ready technical files with tolerance risk notes, inspection plans and DFM recommendations.
TRUMPF TruMatic 6000 combined laser-punching line, Amada turret punching and a dozen welding robots covering laser, arc, TIG/MIG and spot welding.
Long-term supply relationships with machinery importers, distributors and EPC buyers.
Serving machinery importers, distributors and EPC buyers worldwide.
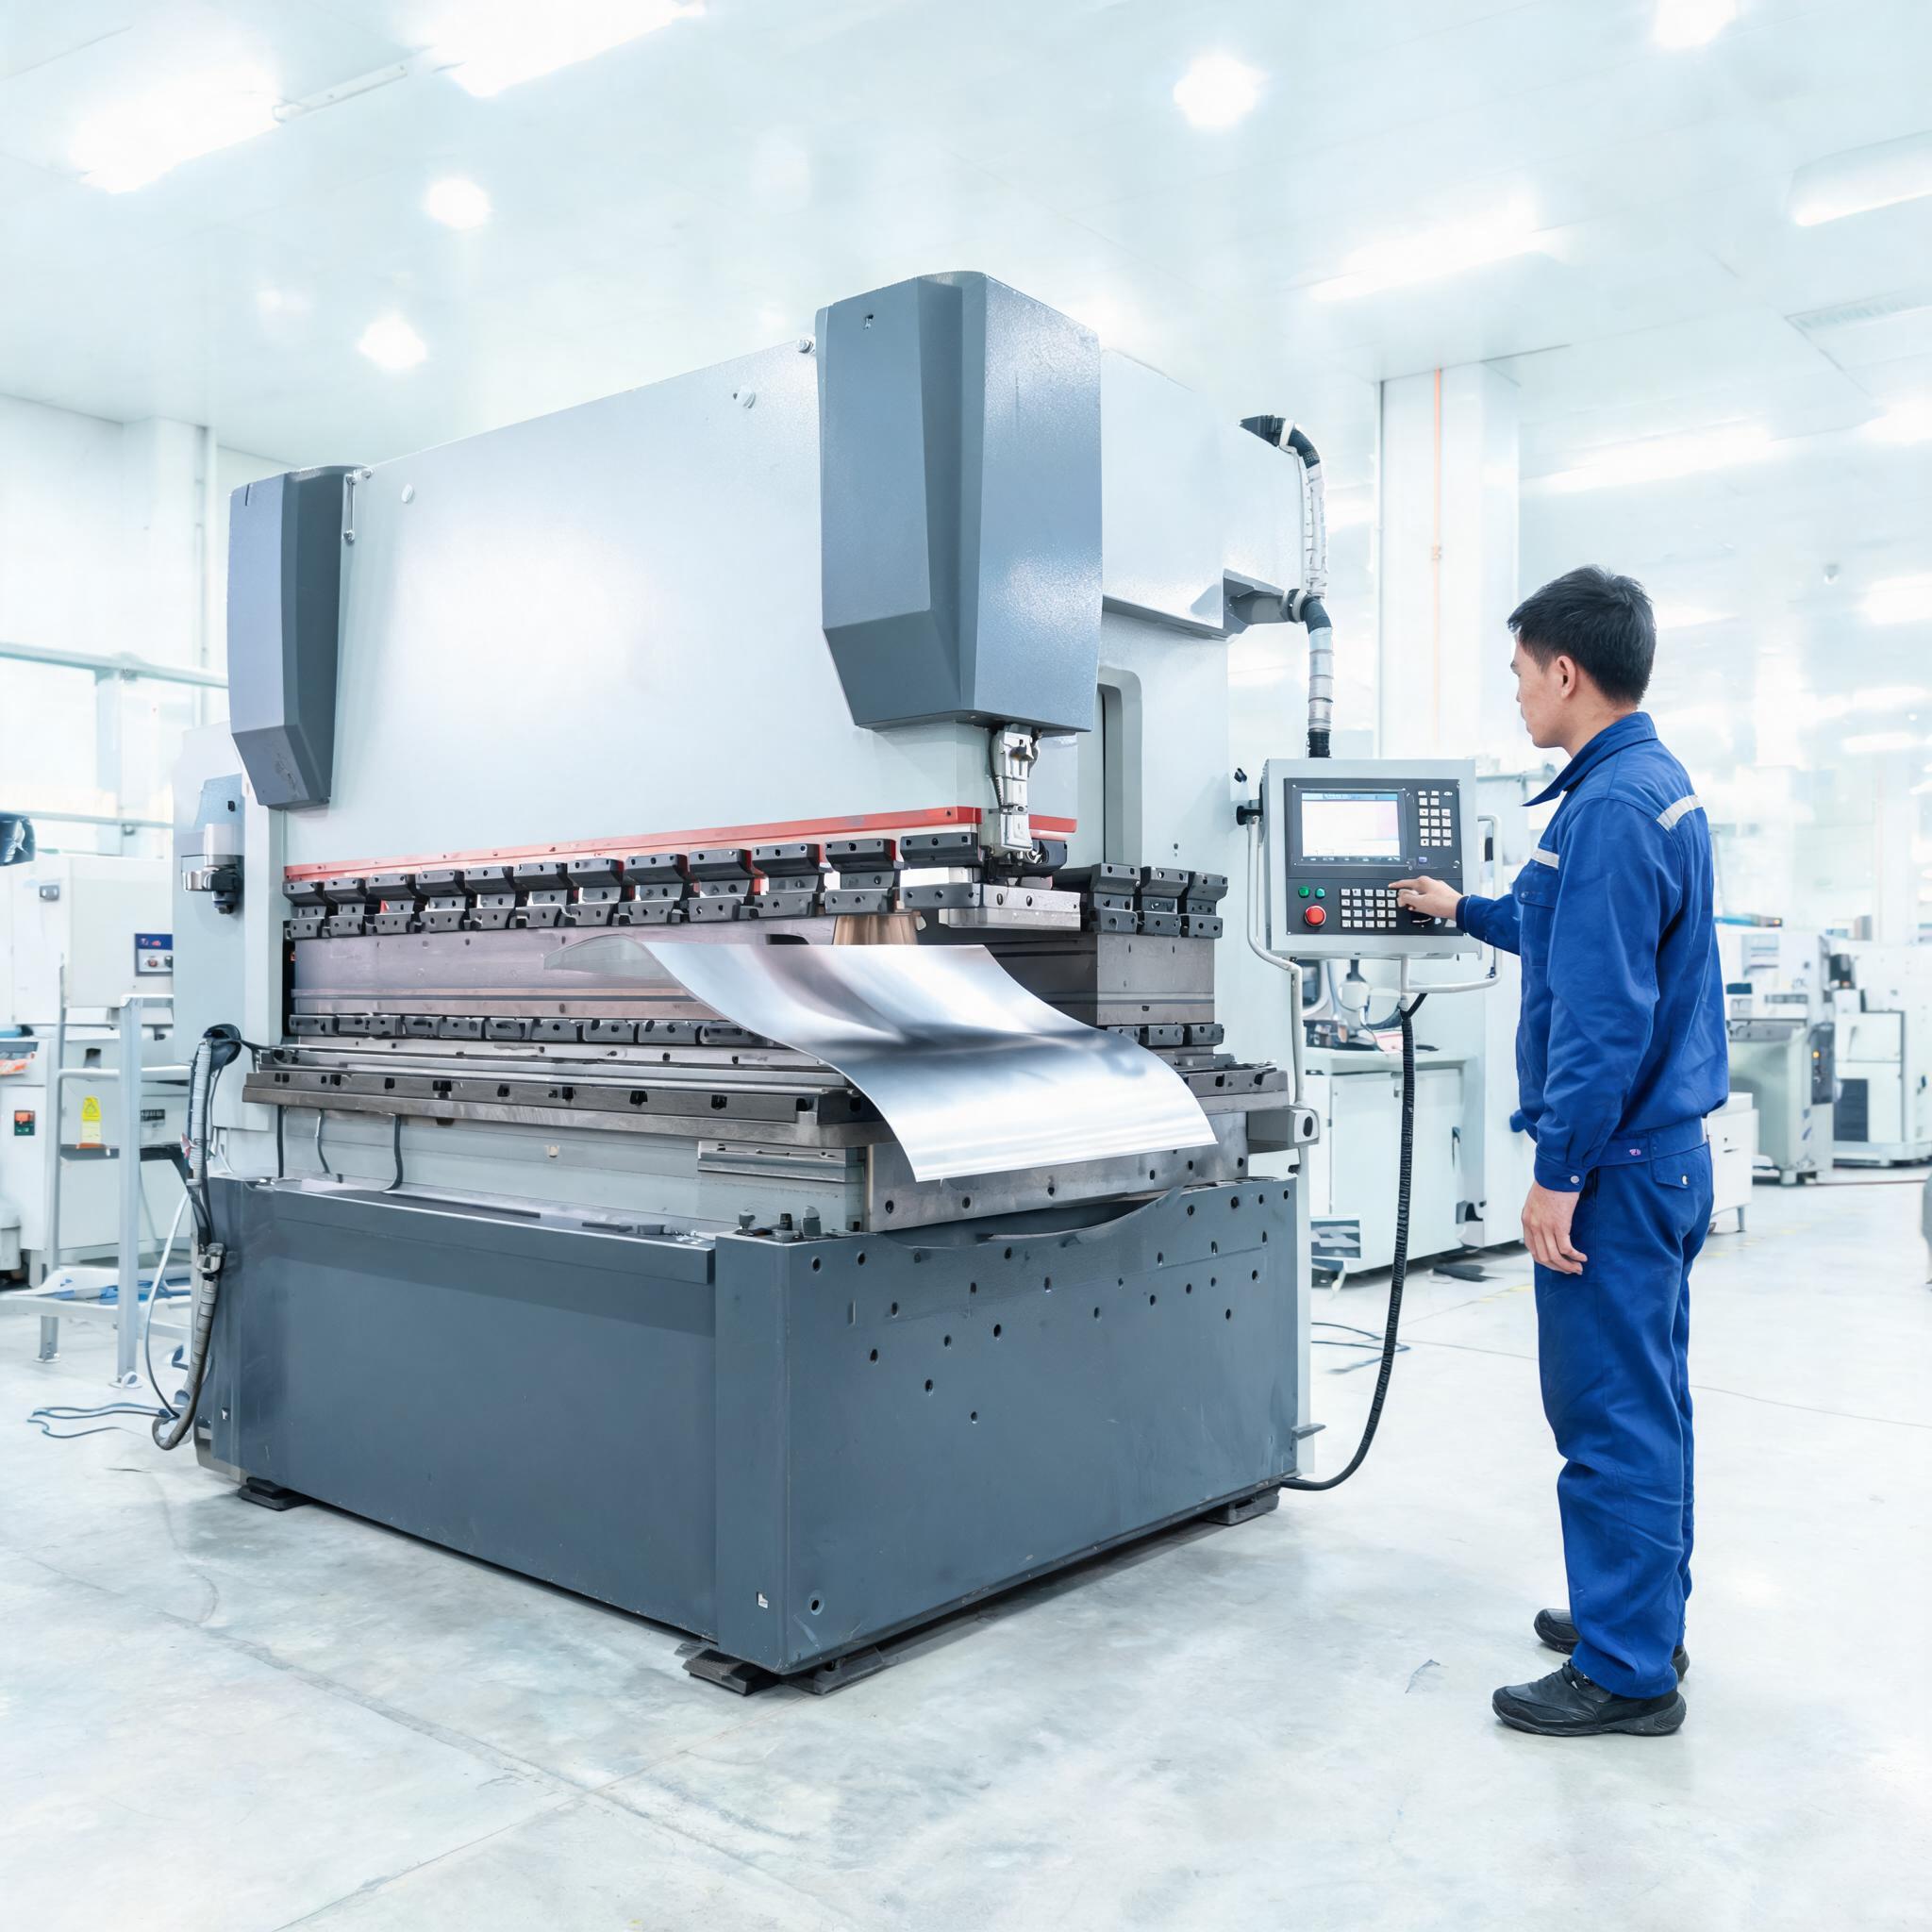
Precision sheet metal bending and forming services. Press brake bending for brackets, enclosures, and structural components. IATF 16949 certified facility serving global machinery buyers.
View service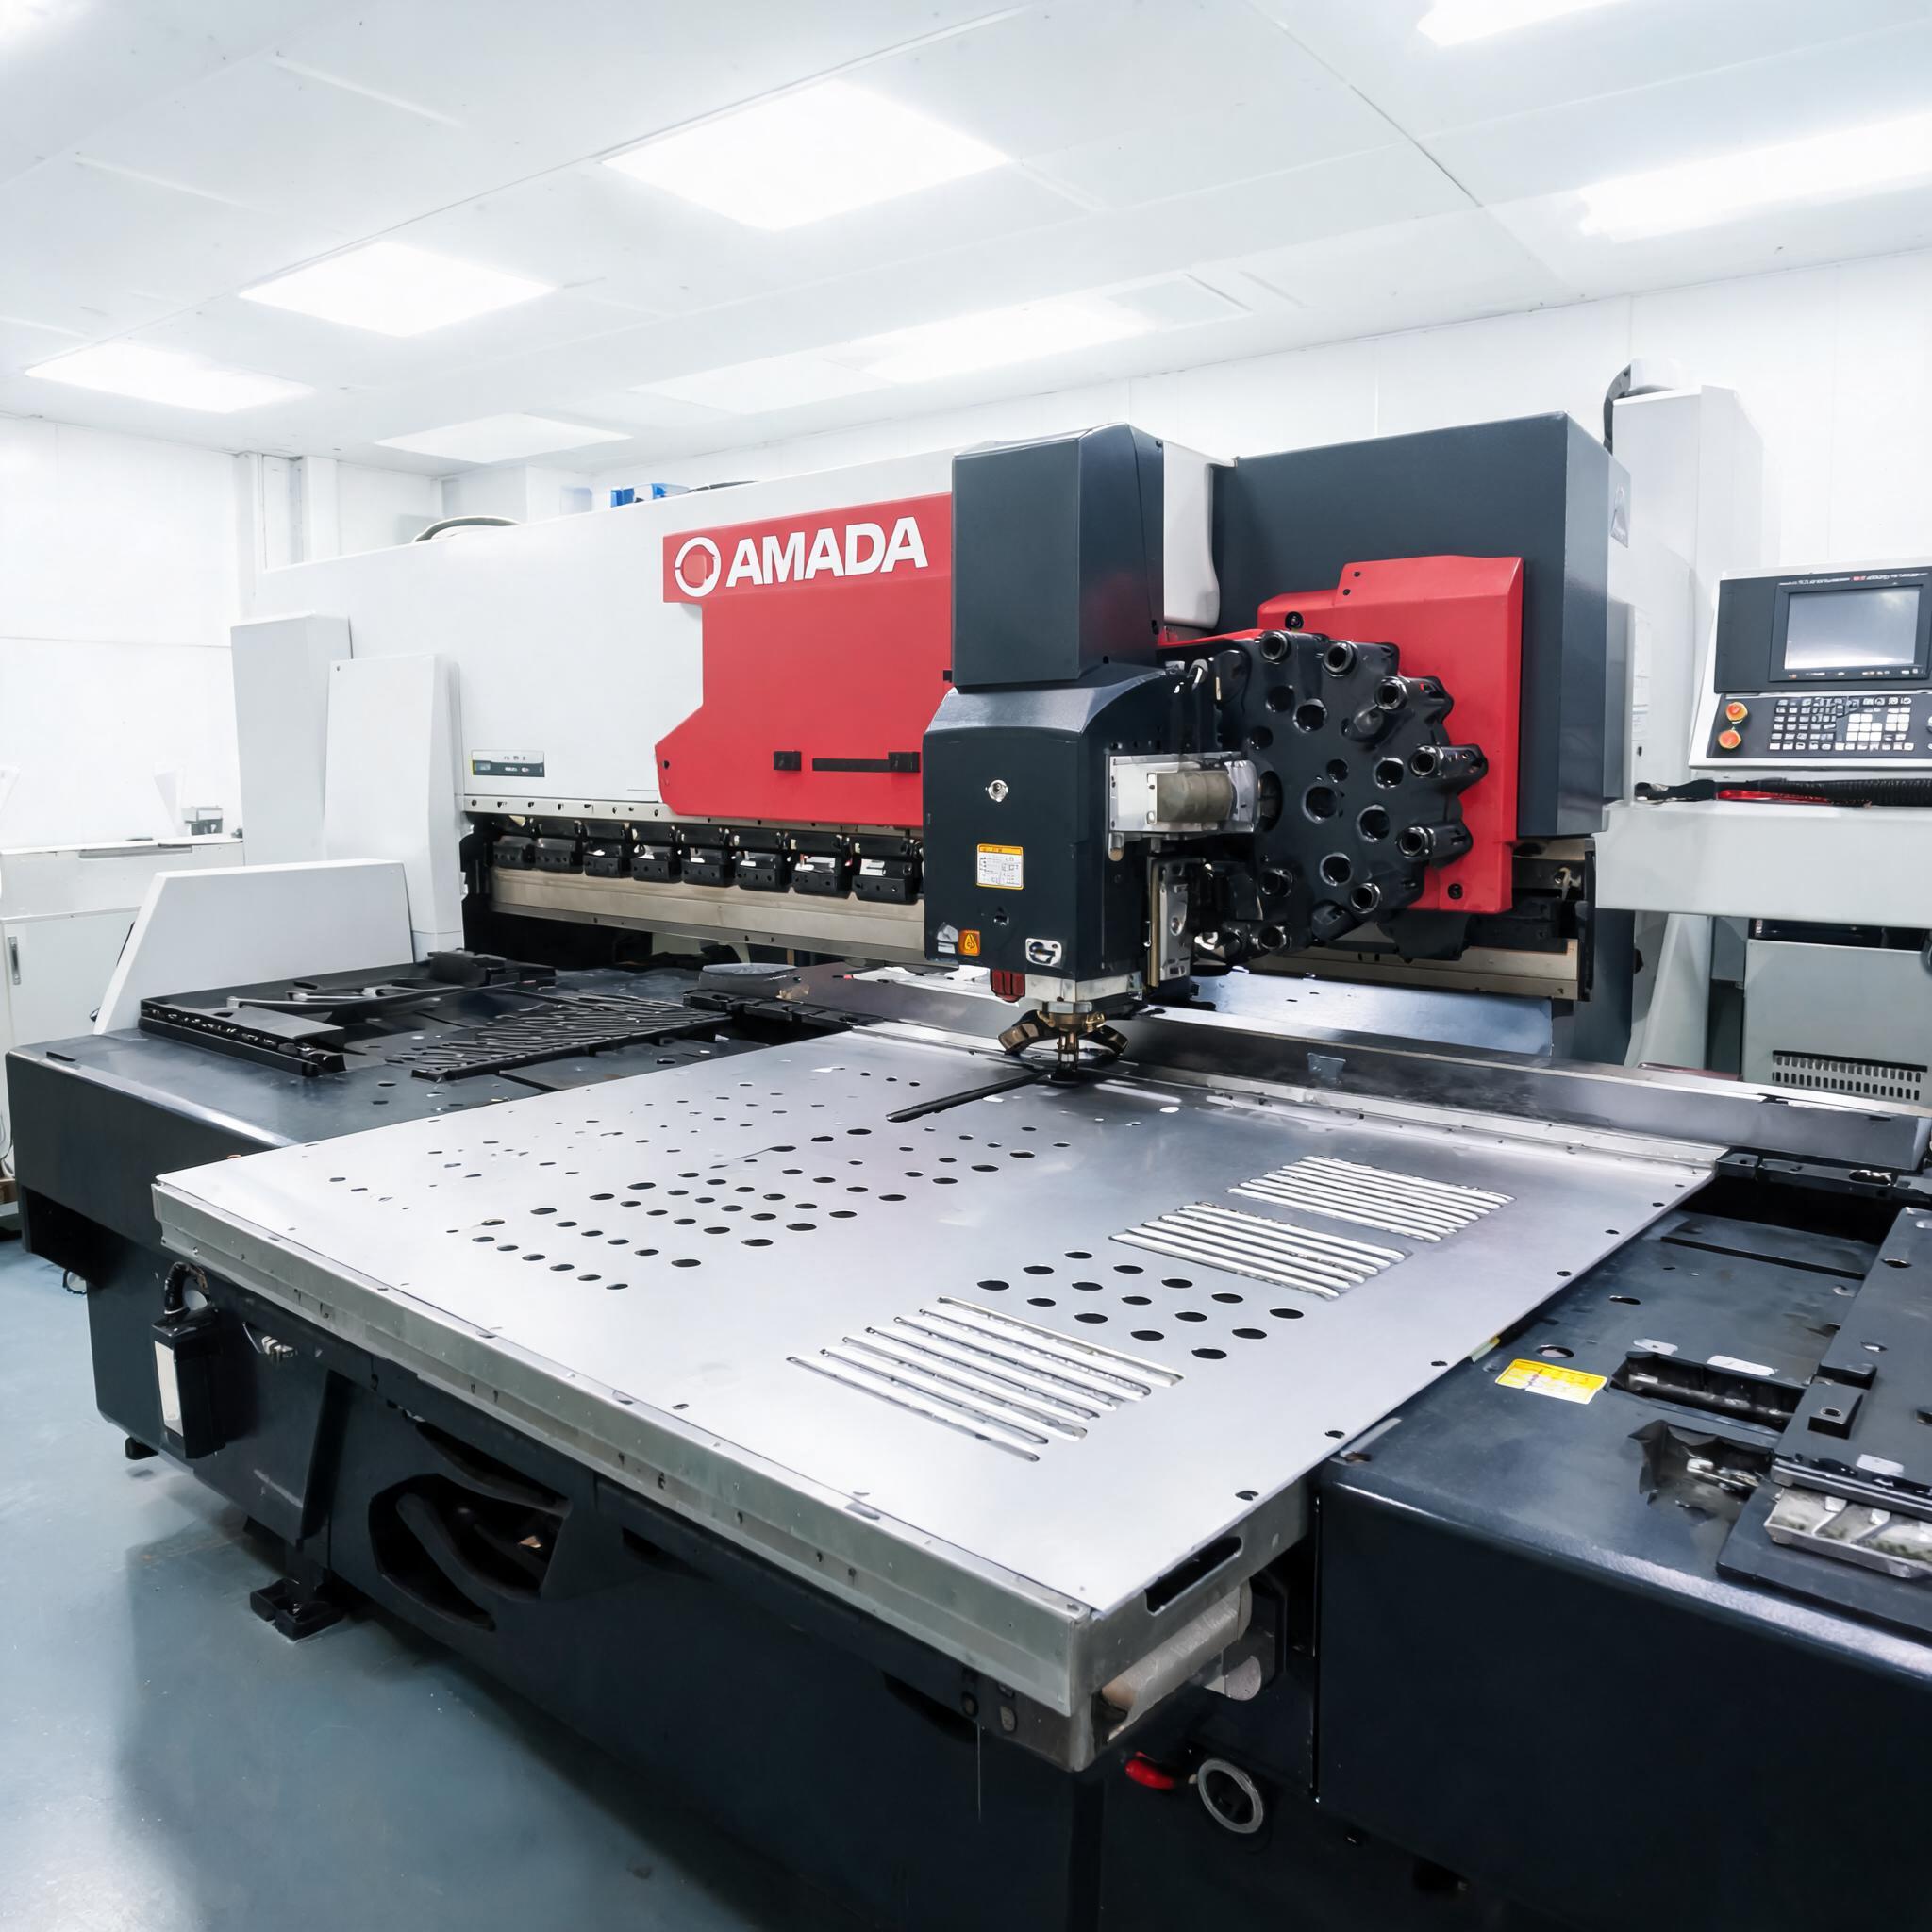
CNC punching and stamping services for sheet metal components. Amada turret punch press and TRUMPF TruMatic 6000. Formed features, louvers, extruded holes and ribs in a single setup. IATF 16949 certified.
View service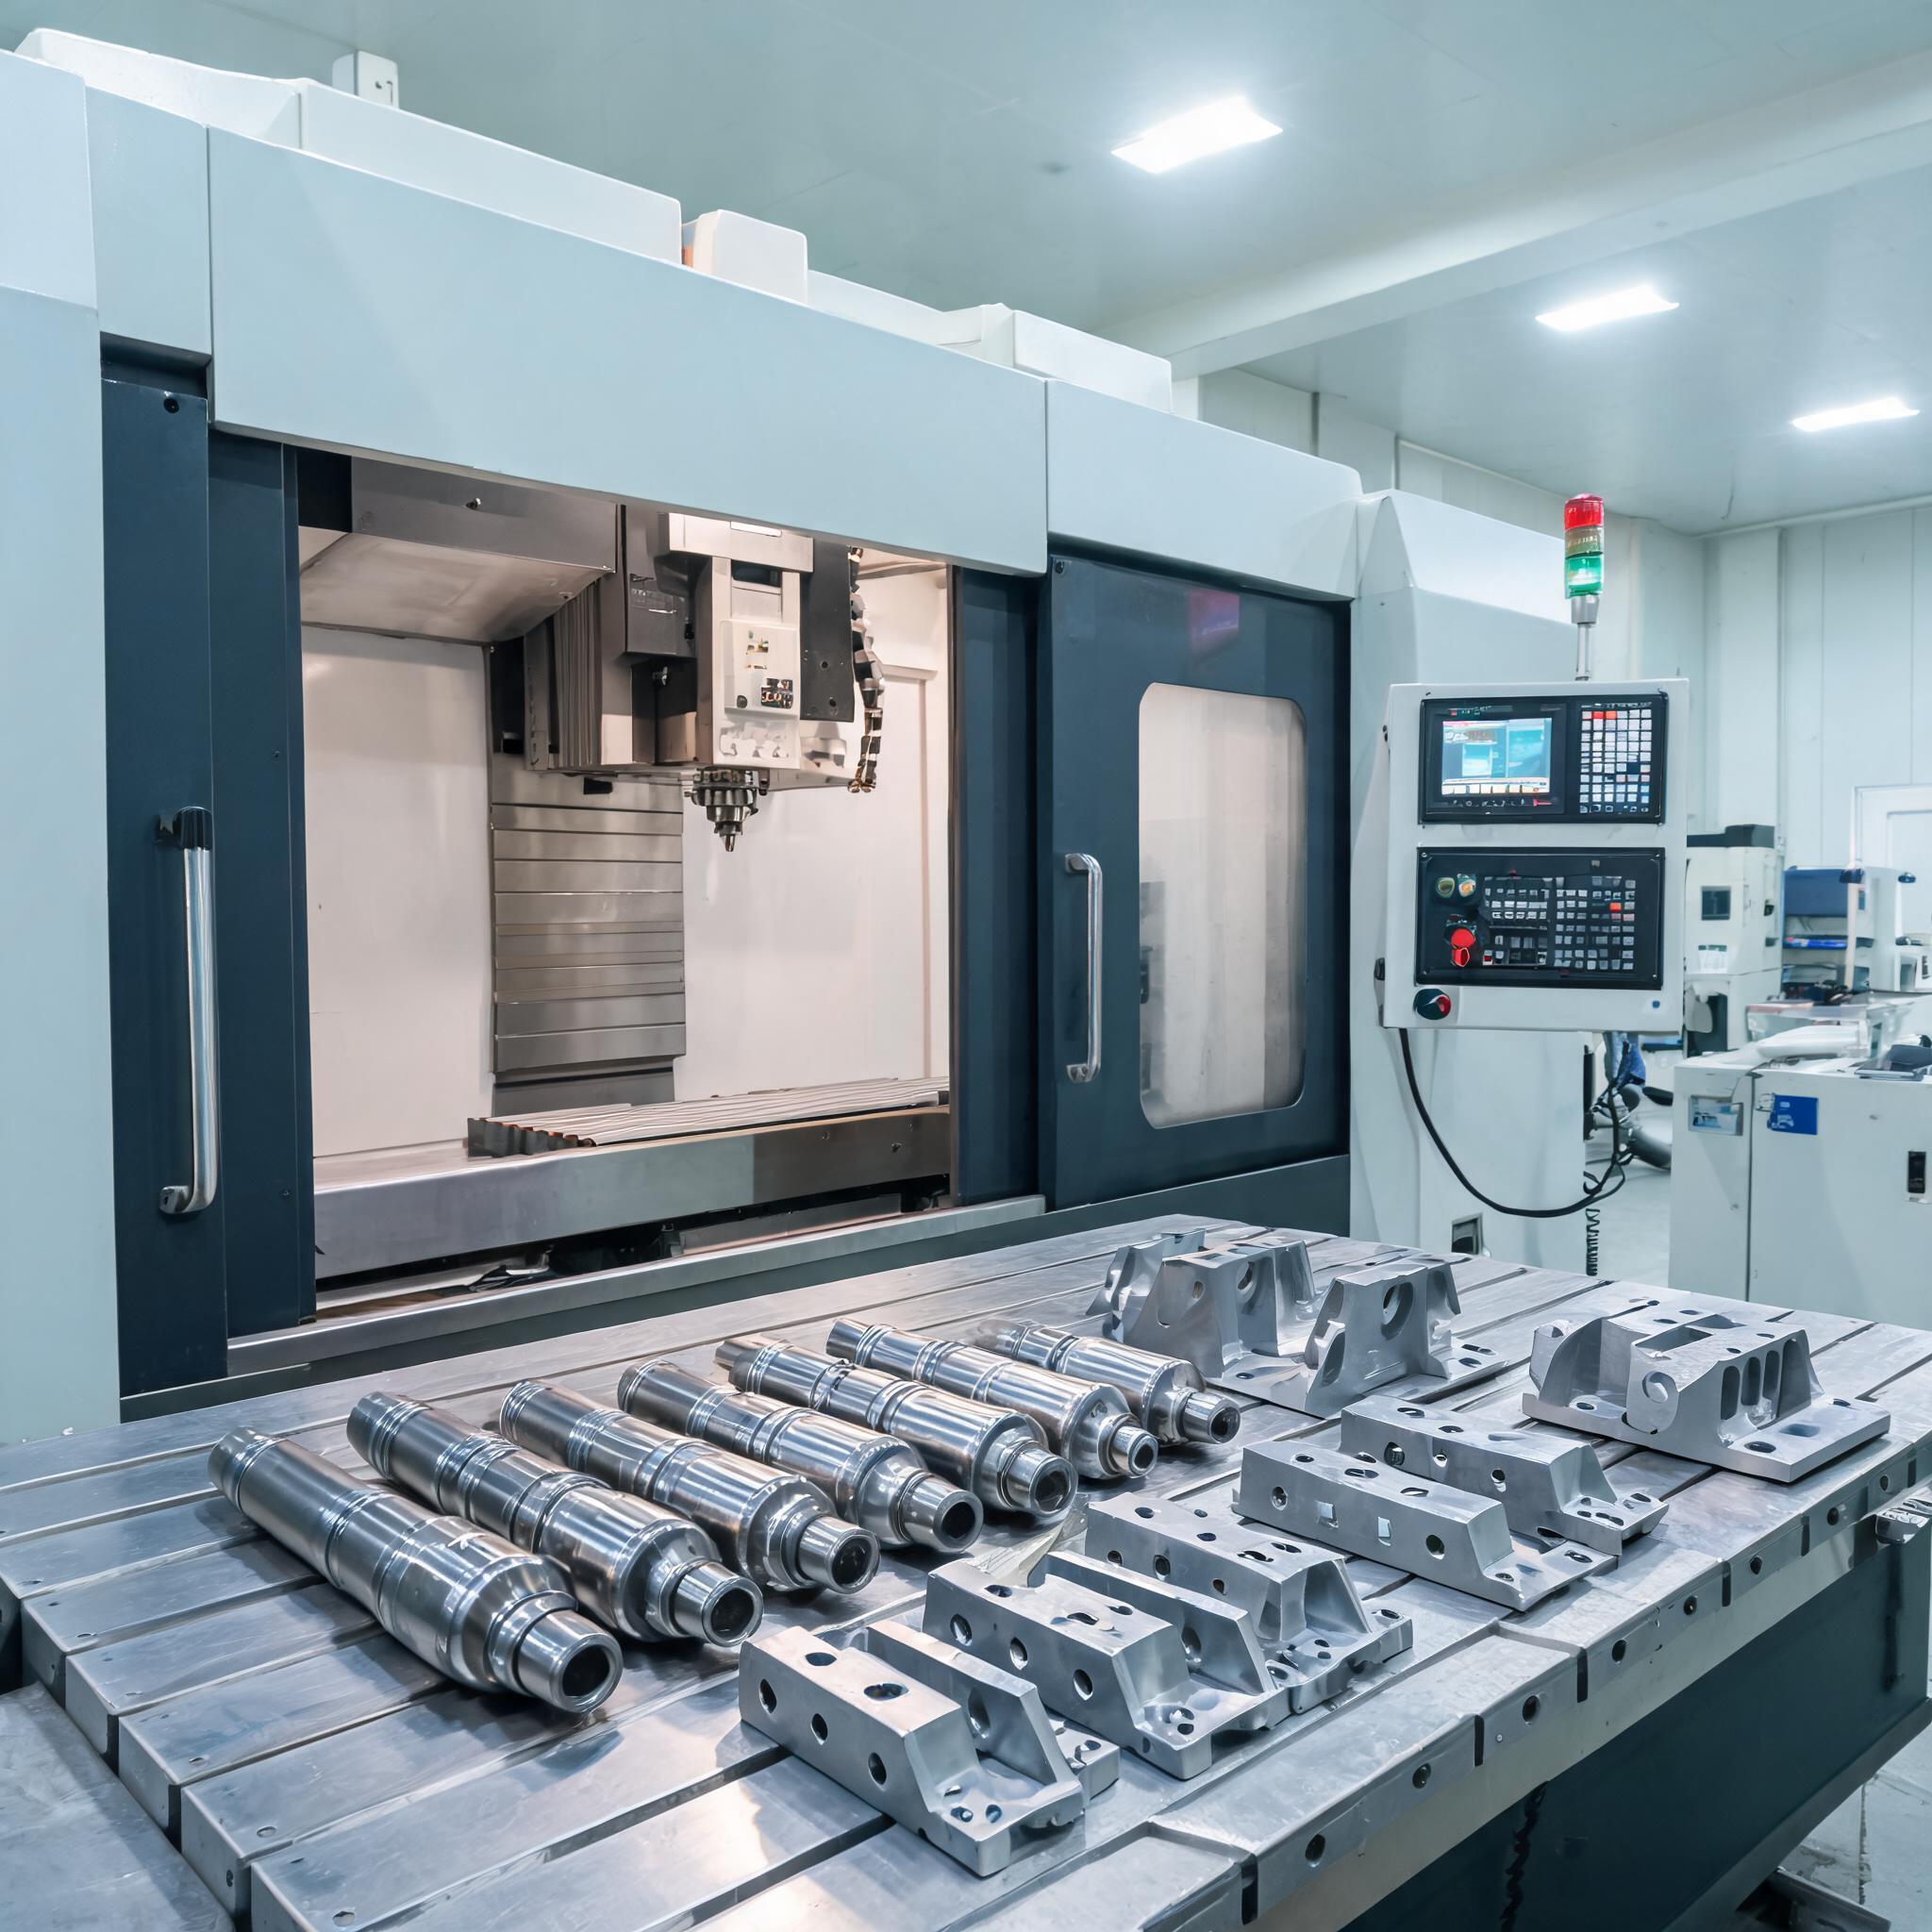
Multi-process precision CNC machining combining turning, milling, drilling and tapping under one roof. IATF 16949 certified turnkey solution for industrial buyers.
View serviceYes — punch tooling and bend sequences are stored per project, and hole positions are verified on first articles before batch release.
Bend radius and grain direction are reviewed at drawing stage; the selector on this page shows general guidance, and final radii are confirmed before production.
Mild steel, stainless steel and aluminum are routine; thickness ranges and tooling limits are confirmed in the quotation.
Yes — finishing scope is written into the inspection plan; coating color and texture are agreed at quotation.
Send drawings with material, thickness, hole pattern and finish expectations. Our engineering team replies with a quote-ready technical file.
Send your drawings, target quantity and application. Submitting this form passes the solution name and this page URL to our sales team, so you do not need to repeat the context.