
Cutouts that arrive in the wrong place
When cutting and forming happen at different shops, cumulative tolerance stack-up moves your connector cutouts and mounting holes — and the components no longer fit.
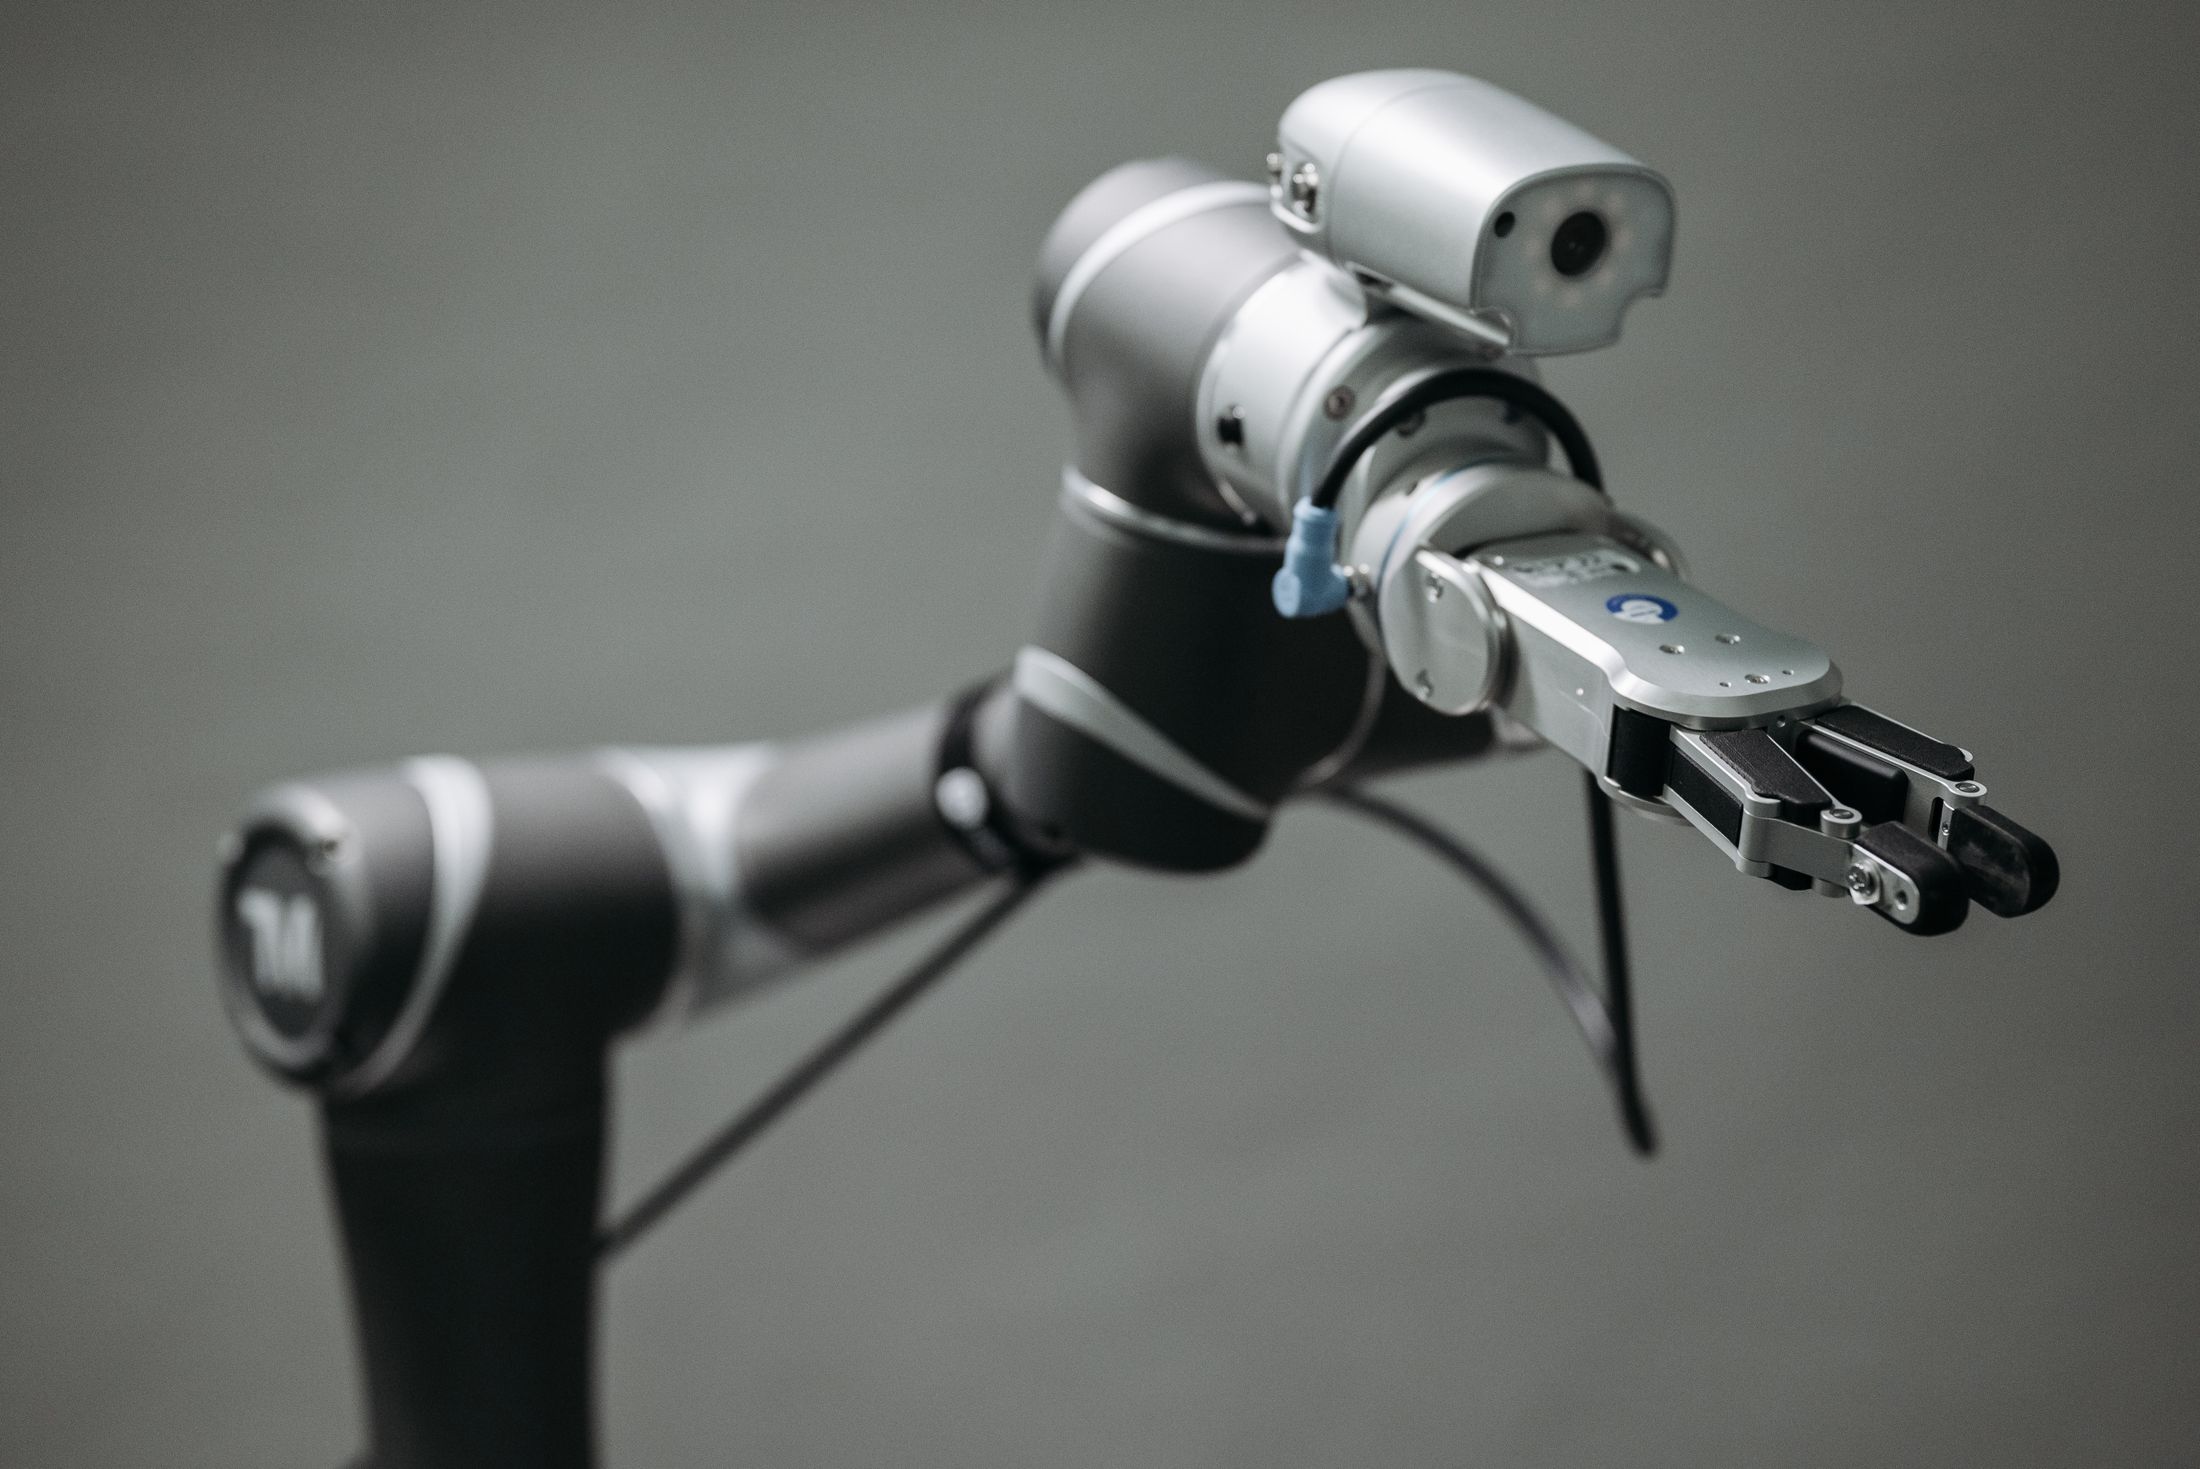
Solution · Sheet Metal Fabrication
An enclosure is never one process — it is cutting, forming, welding and finishing stacked with your cutouts, hardware and tolerances. We run all of them under one roof, so the box that arrives matches the drawing you approved instead of a compromise between four subcontractors.
When cutting and forming happen at different shops, cumulative tolerance stack-up moves your connector cutouts and mounting holes — and the components no longer fit.
Welded frames and boxes warp when heat input is uncontrolled, so doors sag and gaskets leak long before the product ships.
Coating applied over burrs and dents looks fine in photos and fails at installation, costing you rework on site.
Every enclosure project starts with a drawing review where cutout positions, weld sequences and finishing scope are written into the inspection plan. Laser cutting and punching set the geometry, press-brake forming and robotic welding control distortion, and first articles are checked before batch release — under the same roof and the same plan.
TRUMPF TruMatic 6000 combined laser-punching cuts panels and cutouts with tight edge quality.
Press-brake bending with planned bend sequences keeps flange angles repeatable across a batch.
Laser, arc, TIG/MIG and spot welding robots control heat input on frames and seams.
Deburring, coating and hardware installation are scheduled within the same inspection plan.
Select the enclosure family to see the fabrication focus and the checklist our engineering team reviews at drawing stage. Final scope is confirmed in the quotation.
Panels, doors and back plates with accurate cutout arrays; door frames welded for flatness and gasket contact.
Cutout schedule vs. component layout, door gap tolerances, grounding stud positions, finish color and texture.
Typical application examples based on our documented workflow. Buyer roles are anonymized; outcomes depend on project specifics.
Buyer feedback examples framed around our standard documentation and workflow evidence; results reference checkable records.
“The first-article check caught one cutout offset before the batch ran — that single approval saved our assembly week.”
Control manufacturer sourcing cabinets through an industry referral
Verifiable result: First-article approval loop completed before batch release on the referenced project
Source type: FAI report and sample approval record on file
“Hole patterns finally match across shipments, so our assembly jigs stop needing adjustment.”
Telecom integrator consolidating rack and panel supply
Verifiable result: Repeat orders running with sampling-level incoming inspection
Source type: Incoming-inspection records and QC photo packs on file
“Weld flatness was checked and recorded on the first article, which our auditor accepted without follow-up.”
Energy buyer adding housings to an existing machining order
Verifiable result: FAT documentation supplied with the referenced shipment
Source type: FAT record and shipment checklist on file
Certifications below are held by Zhuhai ChunTian Machine Technology Co.,Ltd. Scope and validity details are available with the certificate documents on request.
Operating since 2009 with more than 15 years in precision sheet metal and CNC machining.
300–1,000 staff and an annual revenue of USD 30–150 million, running laser cutting, punching, bending, welding and machining under one roof.
Engineering team turns drawings into quote-ready technical files with tolerance risk notes, inspection plans and DFM recommendations.
TRUMPF TruMatic 6000 combined laser-punching line, Amada turret punching and a dozen welding robots covering laser, arc, TIG/MIG and spot welding.
Long-term supply relationships with machinery importers, distributors and EPC buyers.
Serving machinery importers, distributors and EPC buyers worldwide.
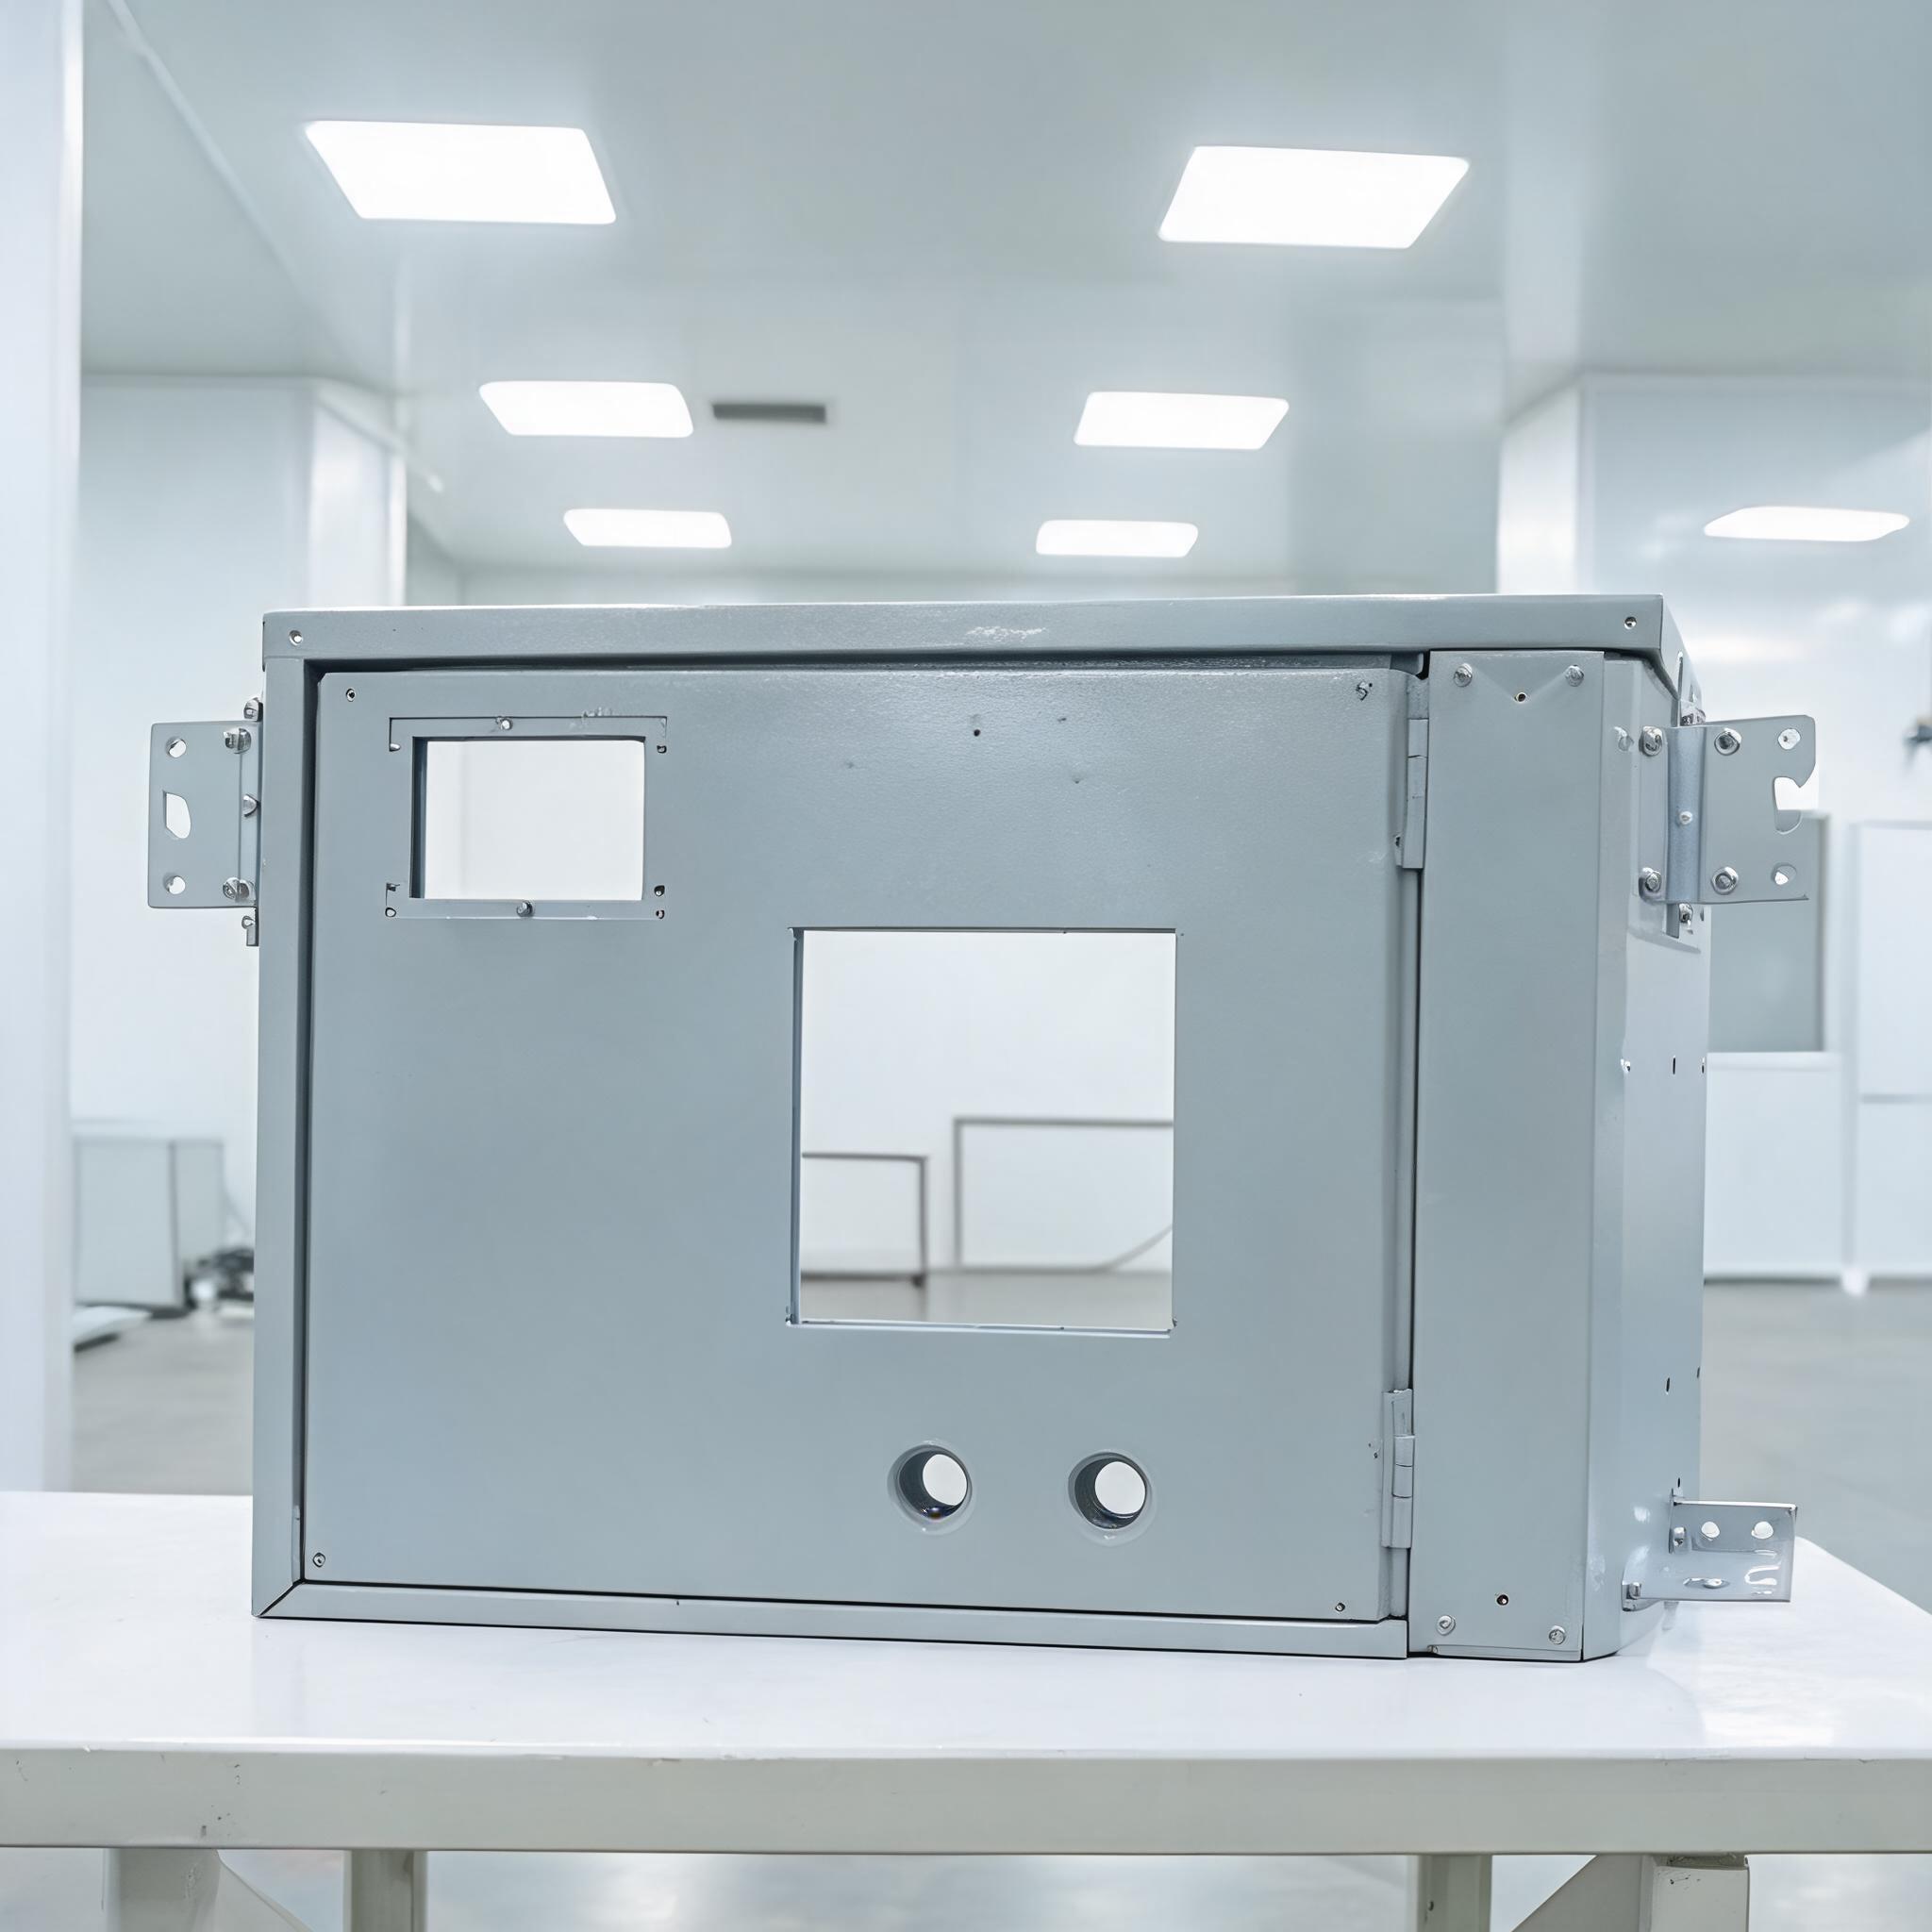
Complete sheet metal enclosure fabrication — laser cutting, punching, bending and welding in one facility. Electrical cabinets, control panels, equipment housings. IATF 16949 certified.
View service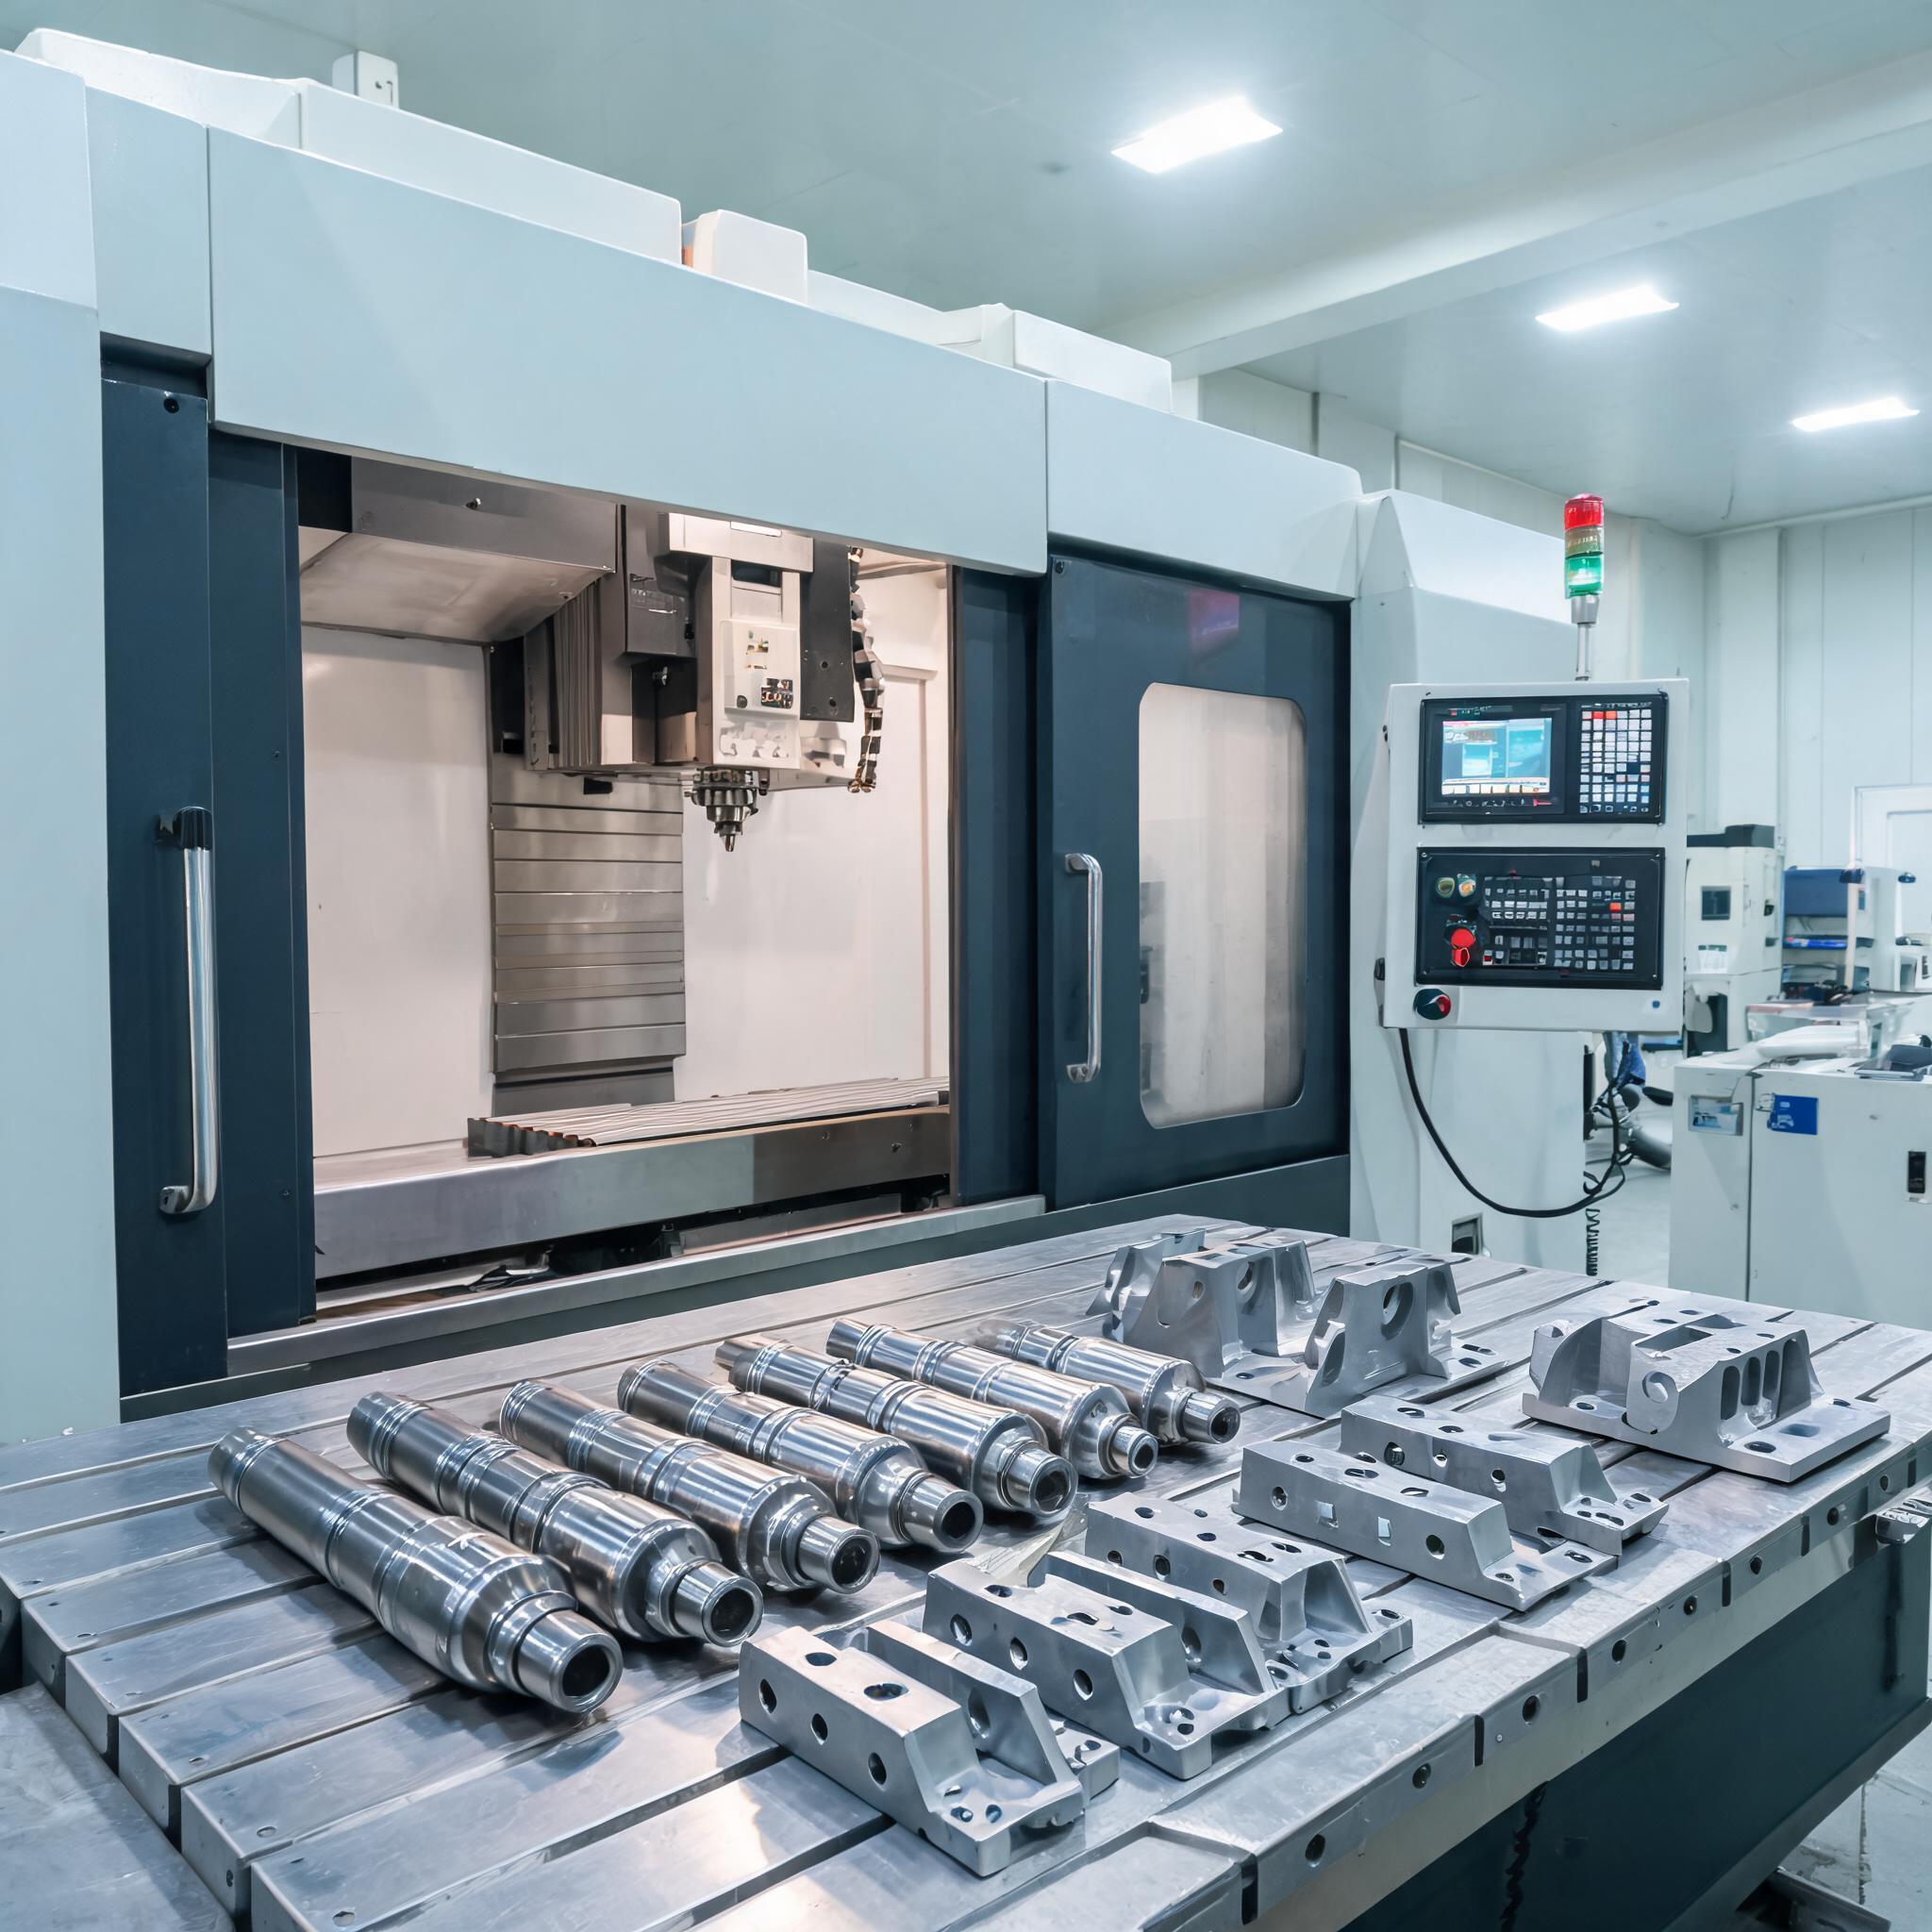
Multi-process precision CNC machining combining turning, milling, drilling and tapping under one roof. IATF 16949 certified turnkey solution for industrial buyers.
View serviceDrawings with cutout schedules, material and thickness, finish expectations and target quantity. Our engineering team replies with a quote-ready technical file.
Yes — cutout positions are reviewed at drawing stage and verified on first articles before batch release.
Weld sequences are planned at drawing review, robotic welding controls heat input, and flatness is checked on first articles.
Deburring, coating and hardware installation are scheduled within the same inspection plan, with the scope written into the quotation.
Sub-assembly and final assembly services are available; scope and packing are confirmed in the quotation and shipment checklist.
Send your drawings, target quantity and application. Submitting this form passes the solution name and this page URL to our sales team, so you do not need to repeat the context.